Packaging speed means very little if cartons keep popping open on the line or in transit. Adhesive application methods for packaging lines matter because the method, not just the glue, decides bond consistency, cleanup time, energy use, and downtime. For Kenyan manufacturers handling cartons, trays, labels, and paper-based packs, the right setup depends on substrate, line speed, temperature, and product exposure. If you want a supplier that understands both hot melt and cold-glue needs in East Africa, Thika Wax Works is a strong place to start.
What packaging lines usually use, and where each method fits best
Most packaging lines rely on hot melt, cold glue, or pressure-sensitive tape, and each method solves a different production problem. Hot melt is common for fast carton sealing and case forming. Cold glue is often chosen for paper, board, labels, and some folding applications where open time matters. Pressure-sensitive tape sticks when pressure is applied and does not need heat or solvent activation, according to the Wikipedia-based definition in the research data.
For busy plants in Nairobi, Thika, Mombasa, or Athi River, the practical question is simple: do you need speed, repositioning time, or easy maintenance? A fast FMCG line may lean toward hot melt, while paper converting or labeling may work better with liquid adhesive. If you are comparing chemistries first, this guide to hot melt adhesives in Kenya for 2026 gives a useful local primer.
Quick comparison table
| Method | How it is applied | Best fit on the line | Main watch-out |
|---|---|---|---|
| Hot melt adhesive | Heated tank, hose, nozzle, bead or spray | Carton sealing, tray forming, high-speed case packing | Temperature control and nozzle char |
| Cold glue | Wheel, disc, nozzle, roller, pattern coat | Paperboard, labels, folding cartons | Drying time and moisture sensitivity |
| Pressure-sensitive tape | Pressure-applied tape head | Case sealing, bundling, rework-friendly lines | Consumable roll changes |
| Filament tape | Reinforced pressure-sensitive tape with fiberglass backing | Heavy packs, strapping support, load stability | Less suited for invisible presentation bonds |
A separate decision comes down to board type and food-contact needs. If you package dry foods, bakery items, or takeaway products, read this guide on safe adhesives for food packaging before changing line settings or adhesive grade.
Hot melt application wins on speed, but only when the pattern and temperature are right
Hot melt works best when you match application pattern, add-on amount, and temperature to the carton and line speed. In packaging, the usual patterns are bead, slot, swirl, and spray. A narrow bead is common for carton flaps, while swirl or spray can help when wider surface coverage is needed without over-applying adhesive.
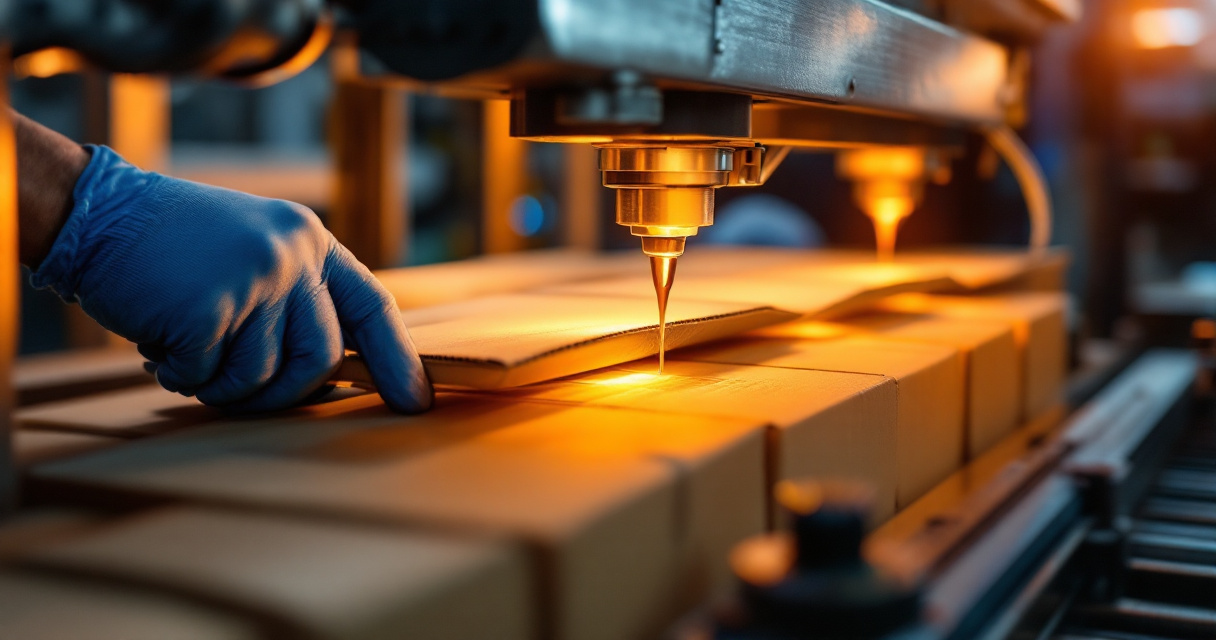
Too much heat can scorch adhesive and clog nozzles. Too little heat can raise viscosity, which makes the bond weak or patchy. That balance matters even more in Kenya where factory conditions can shift between cool mornings and hot afternoons.
The hot melt setup points that affect bond quality
- Tank temperature: Keep within the supplier's recommended range.
- Hose and nozzle temperature: Avoid cold spots that thicken flow.
- Pattern placement: Put adhesive where compression happens, not where board gaps are widest.
- Compression time: Hold long enough for wet-out and set.
- Substrate condition: Dusty or coated surfaces often need testing first.
A lot of line issues blamed on "bad glue" are really application issues. If your cartons are opening at the flap edge, the problem may be bead location, not adhesive chemistry. For more on carton-specific selection, this comparison of hot melt vs cold glue for carton packaging in East Africa is worth reading.
"Quality is never an accident; it is always the result of intelligent effort.", John Ruskin, Quote Investigator reference
Video: how tape and adhesive products are manufactured
That manufacturing view helps line managers understand why adhesive consistency, coating weight, and converting quality affect what happens downstream on a packaging line.
Cold glue and tape methods make sense when heat is a bad fit
Cold glue and pressure-sensitive tape are often the smarter choice when you need simpler equipment, lower application temperature, or cleaner changeovers. Cold glue is widely used on paper and board because it wets porous surfaces well and can be applied by roller, wheel, or nozzle systems. It is especially useful when line speed is moderate and bond formation can rely on water loss or absorption.
Tape is different. Pressure-sensitive tape bonds with applied pressure, and filament tape adds reinforcement through fiberglass strands in a polypropylene or polyester backing, based on the research definitions. On secondary packaging, tape can reduce heated-equipment maintenance, though roll changes and tape-head adjustment still matter.
When to choose cold glue or tape
- Choose cold glue for paperboard jobs where absorbency helps bonding.
- Choose tape when operators need quick startup and easy visual seal checks.
- Choose filament tape for heavier bundled packs that need added tensile support.
- Choose fugitive glue when items must be held temporarily, then separated cleanly.
Temporary holds matter in promos, inserts, and direct-mail style packs too. If that is part of your operation, this article on fugitive glue for marketing materials shows where light-tack systems fit.
One caution: cold glue performance depends heavily on storage, solids balance, and line cleanliness. Tape depends on pressure, surface energy, and proper application angle. Neither method is "plug and play" if your materials or environment keep changing.
How to run a successful adhesive trial on a live packaging line
A good packaging adhesive trial starts before production day, not when the first carton reaches the applicator. One big content gap in competitor pages is trial planning, yet this is where most time and money get lost. You need agreed targets, known variables, and someone responsible for recording results.
For Kenyan factories, trials should reflect real conditions: the actual board grade, real warehouse temperatures, normal operator staffing, and true line speeds. A perfect trial at half-speed tells you very little about Monday morning production.
Trial checklist before the line starts
- Define success clearly: bond strength, appearance, open time, set speed, or cost per pack.
- Confirm machine parameters: temperature, pressure, pump settings, nozzle size, compression time.
- Prepare samples: include actual carton stock, coatings, inks, and pack weights.
- Assign roles: operator, maintenance lead, QA checker, and supplier contact.
- Plan inspection points: right after sealing, after palletizing, and after transport simulation.
What to record during the trial
| Checkpoint | What to observe | Why it matters |
|---|---|---|
| Application pattern | Bead width, skip marks, stringing | Shows whether delivery is stable |
| Bond after compression | Flap seal integrity, squeeze-out | Confirms placement and add-on level |
| 30 to 60 minutes later | Set quality, carton spring-back | Shows practical hold strength |
| End of shift | Nozzle cleanliness, char, buildup | Predicts maintenance load |
| Next-day samples | Seal durability after storage | Catches delayed failures |
If your line uses paper and board heavily, this resource on paper and board adhesives for high-performance bonding helps you frame the right test criteria.
Scholarly manufacturing literature keeps pointing to the same lesson: process design matters as much as material choice. Research on end-to-end system design in advanced materials also supports this broader principle, where material performance depends on the total application setup, not an isolated component alone, as discussed in Nature Reviews Materials.
What to expect in 2027, and how Thika Wax Works can support line decisions now
Packaging adhesive application is moving toward tighter process control, lower waste, and better fit with paper-based packaging growth. That does not mean every Kenyan plant needs a high-end automated upgrade tomorrow. It means buyers should ask better questions now about temperature stability, substrate fit, food-packaging safety, and maintenance load.
You can also expect more demand for lower-temperature systems where energy use and operator safety matter, especially in smaller and mid-sized operations. If that direction fits your plant, this guide to low-temperature hot melt adhesive sticks in Kenya offers a practical next step.
How Thika Wax Works handles this
Thika Wax Works is useful here because many packaging teams do not need theory alone, they need adhesive options that match local operating conditions. That includes hot melt adhesives, liquid cold glues, and support for industrial buyers trying to balance bond quality, machine fit, and cost.
Visit thikawaxworks.com if you want to compare options before your next trial, especially if your plant runs cartons, paperboard packs, or mixed packaging formats. With Thika Wax Works, you can start the discussion around the application method first, then narrow down the adhesive grade that fits your line.
Video: BOPP tape production in action
"However beautiful the strategy, you should occasionally look at the results.", Winston Churchill, International Churchill Society
That quote fits packaging lines well. Your best method is the one that keeps seals consistent at your real production speed, with your actual packs, in your factory conditions.
Conclusion
The best adhesive application methods for packaging lines are the ones that match your substrate, line speed, sealing pattern, and operating conditions, not just the cheapest adhesive on paper. Hot melt suits many fast carton lines, cold glue stays valuable for paper and board, and tape still has a place where simplicity and quick checks matter. The smartest move is to test method, equipment settings, and adhesive grade together.
If you're looking for packaging adhesives in Kenya and want practical guidance before your next production trial, Thika Wax Works has you covered. You can head to thikawaxworks.com for more product information, or get direct help here: https://www.thikawaxworks.com/contact-us/